Check pocket table heidenhain как убрать
Pocket table for tool changer, 2 t ool d a ta – HEIDENHAIN iTNC 530 (340 420) ISO programming User Manual
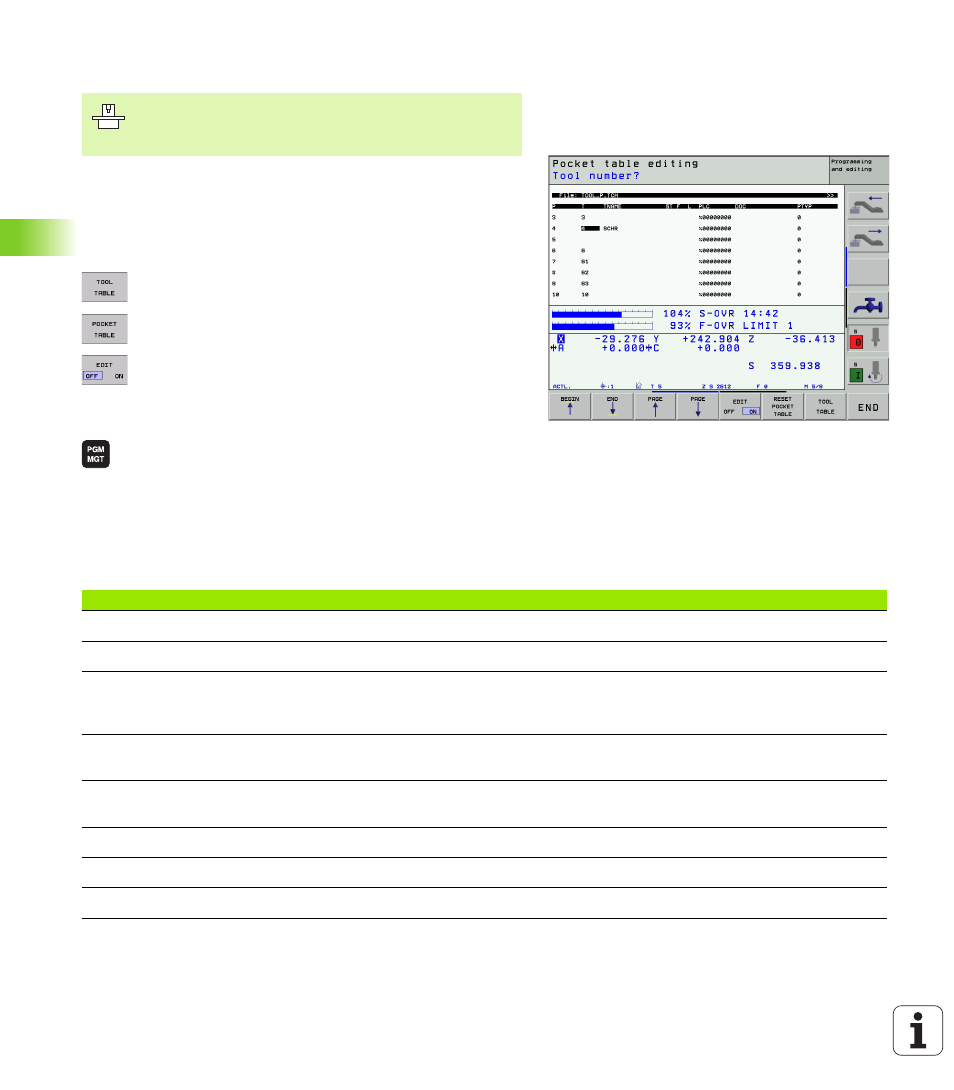
For automatic tool changing you need the pocket table TOOL_P.TCH.
The TNC can manage several pocket tables with any file names. To
activate a specific pocket table for program run you must select it in
the file management of a Program Run mode of operation (status M).
Editing a pocket table in a Program Run operating mode
To select the tool table, press the TOOL TABLE soft
To select the pocket table, press the POCKET TABLE
Set the EDIT soft key to ON.
Selecting a pocket table in the Programming and
Editing operating mode
Call the file manager.
To select the file type, press the SELECT TYPE soft
To show files of the type .TCH, press the soft key TCH
FILES (second soft-key row).
Select a file or enter a new file name. Conclude your
entry with the ENT key or the SELECT soft key.
The machine tool builder adapts the functional range of
the pocket table to the requirements of your machine. The
machine tool manual provides further information.
Pocket number of the tool in the tool magazine
Tool number?
Special tool with a large radius requiring several pockets in the tool magazine. If
your special tool takes up pockets in front of and behind its actual pocket, these
additional pockets need to be locked in column L (status L).
Special tool?
Fixed tool number. The tool is always returned to the same pocket in the tool
magazine
Машинные параметры ITNC 530 и не только
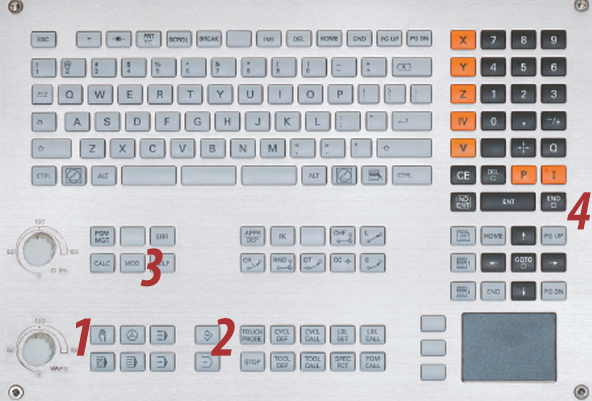
Итак для входа в машинные параматры на системe Heidenhain itnc 530 необходимо нажать следущие клавиши на панеле оператора:
1. Нажимаем кнопку ручного управления «рука» под номером 1.
2. Нажимаем кнопку для входа в режим редактирования под номером 2.
3. Нажимаем кнопку «MOD» под номером 3.
Далее в появившемся окне пишем код для вызова нужной функции из таблицы приведенной ниже
4. После внесения необходимых изменений нажимаем кнопку «END» поод номером 4.
Перезагрузка в большинстве случаев не требуется , и перед изменением любых параметров запишите ,а лучше сфотографируйте старые ,чтобы иметь возможность если ,что пойдет не так вернуть все как было.
Система ЧПУ HEIDENHAIN
Большое количество станкостроительных предприятий оснащают свои станки системами ЧПУ Heidenhain как в базовой комплектации, так и опционально, например, DMG MORI, HERMLE, HURON, FEHLMANN, KOVOSVIT MAS и т.д. Связано это с тем что, данная система имеет широкий ряд систем, начиная с простой и компактной для трёх координатных станков (TNC 320) с возможность управления 2-мя дополнительными осями и заканчивая современной системой ЧПУ TNC 640 (с возможностью программирования до 13-осей плюс шпиндель) отличается оптимизированной системой управления перемещением по траектории, большой скоростью отработки кадра.
Цифровая архитектура и встроенное цифровое управление приводами с интегрированными преобразователями обеспечивают высокую скорость обработки при высочайшей точности выполнения контура, что особенно необходимо при обработке как плоских 2.5D контуров, так и при изготовлении сложных 3D-форм. Динамический контроль столкновений (опция DCM) системы TNC 640 контролирует рабочую зону станка на предмет возможных столкновений рабочих органов станка с узлами станка и элементами оснастки.
Адаптивное управление подачей (опция AFC) автоматически регулирует контурную подачу в зависимости от мощности шпинделя и других технологических параметров, позволяя надежно осуществлять как стандартное, так и высокоскоростное фрезерование, это достигается за счет плавного перемещения как при 3-х, так и 5-и осевом фрезеровании, позволяя оптимизировать время обработки, и вести контроль состояния инструмента.
Так же системы ЧПУ от фирмы Heidenhain имеют возможность для ОЦ фрезерно-токарную функцию, с помощью которой можно выполнять полный цикл изготовления детали сокращая вспомогательное время на переналадку, а также увеличивая возможность автоматизации системы.
Пример моделей станков, которые оснащаются системами управления HEIDENHAIN:
- Фрезерные ОЦ: Hermle C30U, DMU 50, HURON MX10;
Программирование циклов
Программирование циклов в системе ЧПУ HEIDENHAIN не требует особых знаний языка программирования и G – кодов, так как используется программирование открытым текстом (интерактивное программирование). Написание программы сопровождаются простыми вопросами и подсказками графическая поддержка облегчает программирование и предоставляет возможность проверки программы в режиме тестирования. Внутри системы имеется множество встроенных циклов, с помощью которых возможно создавать УП для простых операций и контуров, непосредственно на станке.
В системах ЧПУ фирмы Heidenhain имеется множество токарных циклов и функций не только упрощают работу оператора, но также и повышающих эффективность обработки. Даже самые сложные операции токарной обработки можно легко запрограммировать прямо на станке. Несмотря на многообразие функций фрезерно-токарной обработки, система ЧПУ обеспечивает удобство управления, это и является особенностью систем управления HEIDENHAIN.
Для вызова программных циклов необходимо находясь внутри программы нажать клавишу CYCLE DEF на клавиатуре, после чего на экране отобразятся имеющиеся группы циклов рис. 1.
На примере фрезерного станка HERMLE C30U с системой ЧПУ (iTNC 530) расположение групп циклов будет следующее:
-
Осевые циклы (сверление, резьбофрезерование и т.д.);
Циклы сверления и формирования отверстий
Система управления Heidenhain имеет большое количество стандартных осевых циклов, для получения отверстий и резьб, в зависимости от используемого инструмента и требуемых ТУ для получения отверстия можно легко подобрать нужный цикл.
На примере станка HERMLE C30U с системой ЧПУ (iTNC 530) в группе (сверление, резьба), располагается 3 страницы с осевыми циклами, в общей сложности количество циклов – 17, из них 9 для получения отверстий и 8 циклов для нарезания резьбы, на Рис. 2 приведен пример цикла центрования.
- На первой странице располагаются 7 циклов для получения отверстий:
- CYCL DEF 200 – цикл сверления;
- CYCL DEF 201 – цикл развертывания;
- CYCL DEF 202 – цикл расточки;
- CYCL DEF 203 – цикл универсального сверления;
- CYCL DEF 204 – цикл обратной расточки;
- CYCL DEF 205 – цикл глубокого сверления;
- CYCL DEF 208 – цикл расфрезеровки.
Пример задания цикла центрования, с описанием значений параметров:
CYCL DEF 240 CENTERING
Q200=+2 – БЕЗОПАСНОЕ РАСТОЯНИЕ
Q206=+150 – ПОДАЧА РЕЗАНИЯ
Q211=+0 – ВЫДЕРЖКА ВРЕМЕНИ ВНИЗУ
Q203=+0 – КООРД. ПОВЕРХНОСТИ
Q204=+50 – 2 БЕЗОПАСНОЕ РАССТОЯИЕ
Фрезерные циклы
Система ЧПУ iTNC 530 в общей сложности имеет 6 циклов для обработки цапф, канавок, карманов и располагаются в одноименном пункте. А также 3 цикла для торцевого фрезерования располагаются в группе много проходного фрезерования. Данными циклами можно получить основные виды поверхностей, получаемых при фрезеровании.
Для обработки более сложных контуров со стойки, для программирования пользуются разделом SL циклы, задавая в основной программе, ссылку на метку (подпрограмму) и необходимый цикл, а в самой метке задаются параметры контура.
- Циклы обработки цапф, пазов и карманов:
- CYCL DEF 251 – цикл фрезерования прямоугольного кармана;
- CYCL DEF 252 – цикл фрезерования круглого кармана;
- CYCL DEF 253 – цикл фрезерования прямоугольного паза;
- CYCL DEF 254 – цикл фрезерования кругового паза;
- CYCL DEF 256 – цикл фрезерования прямоугольной цапфы;
- CYCL DEF 257 – цикл фрезерования круговой цапфы.
- Циклы много проходного фрезерования (торцевого):
- CYCL DEF 230 – цикл строчное фрезерование;
- CYCL DEF 231 – цикл линейчатая поверхность;
- CYCL DEF 232 – цикл фрезерования плоскостей.
Пример задания цикла фрезерования прямоугольного паза с описанием его параметров:
CYCL DEF 253 SLOT MILLING
Q215=+0 – ОБЬЁМ ОБРАБОТКИ
Q218=+80 – ДЛИНА ВЫЕМКИ
Q219=+12 – ШИРИНА ВЫЕМКИ
Q368=+0.4 – ПРИПУСК НА СТОРОНЕ
Q374=+0 – ПОЛОЖЕНИЕ ВРАЩЕНИЯ
Q367=+0 – ПОЛОЖЕНИЕ ВЫЕМКИ
Q207=+500 – ПОДАЧА ФРЕЗЕРОВАНИЯ
Q351=+1 – ВИД ФРЕЗЕРОВАНИЯ
Q202=+5 – ГЛУБИНА ВРЕЗАНИЯ
Q369=+0 – ПРИПУСК НА ГЛУБИНЕ
Q206=+150 – ПОДАЧА ВРЕЗАНИЯ НА ГЛУБИНУ
Q338=+0 – СОСТОЯНИЕ ЧИСТОВОЙ ОБРАБОТКИ
Q200=+2 – БЕЗОПАСНОЕ РАССТОЯНИЕ
Q203=+0 – КООРДИНАТА ПОВЕРХНОСТИ
Q204=+50 – 2–Е БЕЗОПАСНОЕ РАССТОЯНИЕ
Q385=+500 – ПОДАЧА ЧИСТОВАЯ ОБРАБОТКА
Токарные циклы
Для программирования токарных операций на примере управления системой ЧПУ Heidenhain CNC PILOT 620 имеется эффективная функция TURN PLUS которая гарантирует быстрое и простое управление: после ввода геометрических параметров, материала и зажимного приспособления.
TURN PLUS автоматически предложит:
-
Создание плана обработки
В конечном результате будет получена программа DIN PLUS с детальными комментариями. TURN PLUS существенно упрощает создание управляющих программ с наклонными контурами. Очень часто бывает, что наклон контура больше, чем угол режущей кромки инструмента. В таких случаях CNC PILOT 620 автоматически, подбирает необходимый инструмент и осуществляет обработку в противоположном направлении, или в случае необходимости в виде выточки.
Ниже приведены основные токарные циклы применяющиеся, для системы ЧПУ Heidenhain TNC 640,
CYCL DEF 810 – цикл чернового продольного точение контура;
CYCL DEF 811 – цикл продольного точение уступа;
CYCL DEF 812 – цикл продольное точение уступа, расширенный;
CYCL DEF 813 – цикл продольного врезания;
CYCL DEF 814 – цикл продольного врезания, расширенное;
CYCL DEF 815 – цикл точения параллельно контура;
CYCL DEF 820 – цикл поперечного чернового точения контура;
CYCL DEF 821 – цикл поперечного точения уступа;
CYCL DEF 822 – цикл поперечного точения уступа, расширенный;
CYCL DEF 823 – цикл поперечного токарного врезания;
CYCL DEF 824 – цикл поперечное токарного врезания, расширенный;
CYCL DEF 830 – цикл черновой обработки параллельно контуру;
CYCL DEF 831 – цикл продольного нарезания резьбы;
CYCL DEF 832 – цикл нарезания резьбы, расширенный;
CYCL DEF 832 – цикл черновой двунаправленной обработки контура;
CYCL DEF 859 – цикл отрезки;
CYCL DEF 860 – цикл радиальной прорезки контура;
CYCL DEF 861 – цикл радиальной прорезки;
CYCL DEF 862 – цикл радиальной прорезки, расширенный;
CYCL DEF 869 – цикл точение прорезным резцом;
CYCL DEF 870 – цикл аксиальной прорезки контура;
CYCL DEF 871 – цикл аксиальной прорезки;
CYCL DEF 872 – цикл аксиальной прорезки, расширенный.
Пример задания токарного цикла поперечного врезания:
Q215=+0 – ОБЬЁМ ОБРАБОТКИ
Q460=+2 – БЕЗОПАСНОЕ РАССТОЯНИЕ
Q491=+75 – ДИАМЕТР НАЧАЛА КОНТУРА
Q492=+0 – НАЧАЛО КОНТУРА ПО Z
Q493=+20 – ДИАМЕТР КОНЦА КОНТУРА
Q494=-5 – КОНЕЦ КОНТУРА ПО Z
Q495=+60 – УГОЛ УКЛОНА
Q463=+3 – MAX. ГЛУБИНА РЕЗАНИЯ
Q478=+0.3 – ПОДАЧА ЧЕРН.ОБРАБОТКИ
Q483=+0.4 – ПРИПУСК НА ДИАМЕТР
Q494=+0.2 – ПРИПУСК ПО Z
Q505=+0.2 – ПОДАЧИ ЧИСТ.ОБРАБОТКИ
Q506=+0 – ВЫРАВНИВАНИЕ КОНТУРА
L X+75.0 Y+0.0 Z+2.0 FMAX M303
Сообщения об ошибках и обработка ошибок
В случае возникновении ошибок, система ЧПУ оповещает в верхнем левом углу красным текстом название ошибки или предупреждения, а также указывает номер ошибки по которому можно найти причина её возникновения. Под окном с программой может быть описана более точная причина возникновения ошибки.
В случае возникновения предупреждающих ошибок, их можно сбросить кнопкой CE на пульте управления. В случае системных ошибок по руководству к станку, или на сайте Heidenhain скачать каталог “Список ошибок” в индивидуальном порядке найти причину возникновения по номеру ошибки и устранить её.
Машинные параметры ITNC 530 и не только
Итак для входа в машинные параматры на системe Heidenhain itnc 530 необходимо нажать следущие клавиши на панеле оператора:
1. Нажимаем кнопку ручного управления «рука» под номером 1.
2. Нажимаем кнопку для входа в режим редактирования под номером 2.
3. Нажимаем кнопку «MOD» под номером 3.
Далее в появившемся окне пишем код для вызова нужной функции из таблицы приведенной ниже
4. После внесения необходимых изменений нажимаем кнопку «END» поод номером 4.
Перезагрузка в большинстве случаев не требуется , и перед изменением любых параметров запишите ,а лучше сфотографируйте старые ,чтобы иметь возможность если ,что пойдет не так вернуть все как было.
Pocket table for tool changer, 2 t ool d a ta – HEIDENHAIN iTNC 530 (340 420) ISO programming User Manual
For automatic tool changing you need the pocket table TOOL_P.TCH.
The TNC can manage several pocket tables with any file names. To
activate a specific pocket table for program run you must select it in
the file management of a Program Run mode of operation (status M).
Editing a pocket table in a Program Run operating mode
To select the tool table, press the TOOL TABLE soft
To select the pocket table, press the POCKET TABLE
Set the EDIT soft key to ON.
Selecting a pocket table in the Programming and
Editing operating mode
Call the file manager.
To select the file type, press the SELECT TYPE soft
To show files of the type .TCH, press the soft key TCH
FILES (second soft-key row).
Select a file or enter a new file name. Conclude your
entry with the ENT key or the SELECT soft key.
The machine tool builder adapts the functional range of
the pocket table to the requirements of your machine. The
machine tool manual provides further information.
Pocket number of the tool in the tool magazine
Tool number?
Special tool with a large radius requiring several pockets in the tool magazine. If
your special tool takes up pockets in front of and behind its actual pocket, these
additional pockets need to be locked in column L (status L).
Special tool?
Fixed tool number. The tool is always returned to the same pocket in the tool
magazine
heidenhain iTNC 530 User Manual
. . .  Numbers Decimal point
Change arithmetic sign
Capture actual position
Skip dialog questions, delete words
Confirm entry and resume dialog
Clear numerical entry or clear TNC error message
Abort dialog, delete program section
TNC Model, Software and Features
This manual describes functions and features provided by TNCs as of the following NC software numbers.
NC software number
The suffix E indicates the export version of the TNC. The export version of the TNC has the following limitations:
Linear movement is possible in no more than 4 axes simultaneously.
The machine tool builder adapts the useable features of the TNC to his machine by setting machine parameters. Some of the functions described in this manual may not be among the features provided by your machine tool.
TNC functions that may not be available on your machine include:
Probing function for the 3-D touch probe
Tool measurement with the TT 130
Returning to the contour after an interruption
HEIDENHAIN iTNC 530
In addition, the iTNC 530 also has two software option packets that can be enabled by you or your machine tool builder:
Software option 1
Cylinder surface interpolation (Cycles 27 and 28)
Feed rate in mm/min on rotary axes: M116
Tilting the machining plane (Cycle 19 and 3D-ROT soft key in the manual operating mode)
Circle in 3 axes (with tilted working plane)
Software option 2
Block processing time 0.5 ms instead of 3.6 ms
5 axis interpolation
M114: Automatic compensation of machine geometry when working with tilted axes
M128: Maintaining the position of the tool tip when positioning with tilted axes (TCPM)
M144: Compensating the machine’s kinematic configuration for ACTUAL/NOMINAL positions at end of block
Additional parameters finishing/roughing and tolerance for rotary axes in Cycle 32 (G62)
LN blocks (3-D compensation)
Please contact your machine tool builder to become familiar with the features of your machine.
Many machine manufacturers, as well as HEIDENHAIN, offer programming courses for the TNCs. We recommend these courses as an effective way of improving your programming skill and sharing information and ideas with other TNC users.
Touch Probe Cycles User’s Manual:
All of the touch probe functions are described in a separate manual. Please contact HEIDENHAIN if you require a copy of this User’s Manual. ID number: 369 280-xx.
Location of use
The TNC complies with the limits for a Class A device in accordance with the specifications in EN 55022, and is intended for use primarily in industrially-zoned areas.
New features of the NC software 340 420-xx
Connecting the TNC to Windows networks via Ethernet (see “Network settings specific to the device” on page 454)
Definition of overlapping contours with contour formula (see “SL Cycles with Contour Formula” on page 321)
Stepwise magnification/reduction in the test graphic (see “Rotating and magnifying/reducing the 3-D view” on page 425)
The additional status display was expanded to display the active datum table and the active datum number (see “Coordinate transformations” on page 11).
Find/Replace any text (see “The TNC search function” on page 70)
Changing the position of the current block on the screen (see “Editing a program” on page 67)
New Q parameter functions: Check sign and Calculate modulo value when entering formulas (see “Entering Formulas Directly” on page 404)
Generating a file with version numbers (see “Code Numbers” on page 445)
Plunging feed rate for infeed for finishing new in Cycles 210 and 211 (see “SLOT (oblong hole) with reciprocating plunge-cut (Cycle 210),” page 281 and see “CIRCULAR SLOT (oblong hole) with reciprocating plunge-cut (Cycle 211),” page 283)
HEIDENHAIN iTNC 530
Changed features of the NC software 340 420-xx
Cycle 32 Tolerance was expanded so that different filter settings can be selected for High Speed Cutting (HSC) (see “TOLERANCE (Cycle 32)” on page 359).
In Cycle 210 (Slot with reciprocating plunge), the approach behavior for finishing was changed (see “SLOT (oblong hole) with reciprocating plunge-cut (Cycle 210)” on page 281).
The additional status display was expanded to display the active status of program section repeats and subprogram calls.(see “Program section repeats/subprograms” on page 12)
When contents of Q parameters are checked, 16 parameters are now shown in a separate window.(see “Checking and Changing Q Parameters” on page 386)
The number of contour elements permitted in SL Cycles, Group II, has been increased from approx. 256 to approx. 1024 (see “SL Cycles” on page 294).
The transfer of the current tool position coordinates into the program has been improved (see “Actual position capture” on page 66).
The transfer of the value that is calculated by using the on-screen pocket calculator into the program has been modified (see “Integrated Pocket Calculator” on page 80).
Detail magnification is now also possible in plan view (see “Magnifying details” on page 426).
When program sections are copied, the copied block remains highlighted after having been inserted (see “Marking, copying, deleting and inserting program sections” on page 69).
New/changed descriptions in this manual
Meaning of software numbers after the MOD functions have been selected (see “Software Numbers and Option Numbers” on page 444).
Connecting the iTNC directly with a Windows PC (see “Connecting the iTNC directly with a Windows PC” on page 451)
HEIDENHAIN iTNC 530
Manual Operation and Setup
Positioning with Manual Data Input
Programming: Fundamentals of File
Management, Programming Aids
Programming: Programming Contours
Programming: Miscellaneous Functions
Programming: Subprograms and
Program Section Repeats
Programming: Q Parameters
Test Run and Program Run
Tables and Overviews
HEIDENHAIN iTNC 530
Programming: HEIDENHAIN conversational and ISO formats .
Visual Display Unit and Keyboard .
Visual display unit
Modes of Operation .
Manual Operation and Electronic Handwheel
Positioning with Manual Data Input (MDI) .
Programming and editing .
Program Run, Full Sequence and Program Run, Single Block .
“General” status display .
Additional status displays .
Accessories: HEIDENHAIN 3-D Touch Probes and Electronic Handwheels .
3-D touch probes .
HR electronic handwheels .
2 Manual Operation and Setup
2.1 Switch-on, Switch-O ff
2.2 Moving the Machine Axes .
To traverse with the machine axis direction buttons:
Traversing with the HR 410 electronic handwheel .
Incremental jog positioning
2.3 Spindle Speed S, Feed Rate F and Miscellaneous Functions M .
Changing the spindle speed and feed rate
2.4 Datum Setting (Without a 3-D Touch Probe) .
HEIDENHAIN iTNC 530
2.5 Tilting the Working Plane
Traversing the reference points in tilted axes .
Setting the datum in a tilted coordinate system .
Datum setting on machines with rotary tables .
Position display in a tilted system .
Limitations on working with the tilting function .
To activate manual tilting:
3 Positioning with Manual Data Input (MDI)
3.1 Programming and Executing Simple Machining Operations 30.
Positioning with manual data input (MDI) .
Protecting and erasing programs in $MDI .
. 4 Fundamentals of NC, File Management, Programming Aids, Pallet Management
Position encoders and reference marks .
Reference system on milling machines .
Absolute and incremental workpiece positions .
Setting the datum .
4.2 File Management: Fundamentals .
4.3 Standard File Management .
Calling the file manager .
Selecting a file .
Deleting a file .
Data transfer to or from an external data medium .
Selecting one of the last 10 files selected .
Renaming a file
Protect file / Cancel file protection
4.4 Advanced File Management .
Overview: Functions of the expanded file manager .
Calling the file manager
Selecting drives, directories and files .
Creating a new directory (only possible on the drive TNC:\)
Copying a single file .
Copying a directory .
Choosing one of the last 10 files selected. .
Deleting a file .
Deleting a directory .
Renaming a file .
Data transfer to or from an external data medium .
Copying files into another directory .
The TNC in a Network .
4.5 Creating and Writing Programs .
Organization of an NC program in HEIDENHAIN conversational format. .
Defining the blank form – BLK FORM .
Creating a new part program
Programming tool movements in conversational format .
Actual position capture .
Editing a program
The TNC search function .
4.6 Interactive Programming Graphics .
To generate/not generate graphics during programming: .
Generating a graphic for an existing program .
Block number display ON/OFF .
To erase the graphic: .
Magnifying or reducing a detail .
4.7 Structuring Programs
Definition and applications .
To display the program structure window / change the active window: .
To insert a structuring block in the (left) program window .
Selecting blocks in the program structure window .
HEIDENHAIN iTNC 530
4.8 Adding Comments .
Entering comments during programming
Inserting comments after program entry
Entering a comment in a separate block .
Functions for editing of the comment .
4.9 Creating Text Files .
Opening and exiting text files .
Erasing and inserting characters, words and lines .
Editing text blocks .
Finding text sections .
4.10 Integrated Pocket Calculator .
4.11 Immediate Help for NC Error Messages .
Displaying error messages .
4.12 Pallet Management .
Selecting a pallet table .
Leaving the pallet file .
Executing the pallet file .
4.13 Pallet Operation with Tool-Oriented Machining .
Selecting a pallet file .
Setting up the pallet file with the entry form .
Sequence of tool-oriented machining .
To leave the pallet file: .
Executing the pallet file .
5 Programming: Tools
5.1 Entering Tool-Related Data .
Spindle speed S
Requirements for tool compensation .
Tool numbers and tool names .
Delta values for lengths and radii
Entering tool data into the program .
Entering tool data in tables
Pocket table for tool changer .
Calling tool data
5.3 Tool Compensation
Tool length compensation .
Tool radius compensation .
5.4 Three-Dimensional Tool Compensation .
Definition of a normalized vector
Permissible tool forms .
Using other tools: Delta values .
3-D compensation without tool orientation .
Face Milling: 3-D compensation with and without tool orientation .
Peripheral milling: 3-D radius compensation with workpiece orientation .
5.5 Working with Cutting Data Tables .
Table for workpiece materials .
Table for tool cutting materials .
Table for cutting data .
Data required for the tool table .
Working with automatic speed/feed rate calculation .
Changing the table structure .
Data transfer from cutting data tables .
Configuration file TNC.SYS
HEIDENHAIN iTNC 530
6 Programming: Programming Contours
6.1 Tool Movements .
FK Free Contour Programming
Miscellaneous functions M .
Subprograms and Program Section Repeats .
Programming with Q parameters .
6.2 Fundamentals of Path Functions .
Programming tool movements for workpiece machining
6.3 Contour Approach and Departure .
Overview: Types of paths for contour approach and departure .
Important positions for approach and departure
Approaching on a straight line with tangential connection: APPR LT .
Approaching on a straight line perpendicular to the first contour point: APPR LN .
Approaching on a circular path with tangential connection: APPR CT .
Approaching on a circular arc with tangential connection from a straight line to the contour: APPR LCT .
Departing on a straight line with tangential connection: DEP LT .
Departing on a straight line perpendicular to the last contour point: DEP LN .
Departure on a circular path with tangential connection: DEP CT .
Departing on a circular arc tangentially connecting the contour and a straight line: DEP LCT .
6.4 Path Contours—Cartesian Coordinates .
Overview of path functions .
Straight line L .
Inserting a chamfer CHF between two straight lines .
Corner rounding RND .
Circle center CC .
Circular path C around circle center CC .
Circular path CR with defined radius .
Circular path CT with tangential connection .
6.5 Path Contours—Polar Coordinates .
Polar coordinate origin: Pole CC .
Straight line LP .
Circular path CP around pole CC .
Circular path CTP with tangential connection .
6.6 Path Contours—FK Free Contour Programming .
Graphics during FK programming .
Initiating the FK dialog .
Free programming of straight lines .
Free programming of circular arcs .
6.7 Path Contours—Spline Interpolation .
HEIDENHAIN iTNC 530
. 7 Programming: Miscellaneous-Functions
7.1 Entering Miscellaneous Functions M and STOP .
7.2 Miscellaneous Functions for Program Run Control, Spindle and Coolant
7.3 Miscellaneous Functions for Coordinate Data .
Programming machine-referenced coordinates: M91/M92 .
Activating the most recently entered datum: M104
Moving to position in an non-tilted coordinate system with a tilted working plane: M130 .
7.4 Miscellaneous Functions for Contouring Behavior
Smoothing corners: M90 .
Insert rounding arc between straight lines: M112 .
Do not include points when executing non-compensated line blocks: M124 .
Machining small contour steps: M97 .
Machining open contours: M98
Feed rate factor for plunging movements: M103 .
Feed rate in millimeters per spindle revolution: M136 .
Feed rate at circular arcs: M109/M110/M111 .
Calculating the radius-compensated path in advance (LOOK AHEAD): M120 .
Superimposing handwheel positioning during program run: M118 .
Retraction from the contour in the tool-axis direction: M140 .
Suppressing touch probe monitoring: M141 .
Delete modal program information: M142 .
Delete basic rotation: M143 .
7.5 Miscellaneous Functions for Rotary Axes .
Feed rate in mm/min on rotary axes A, B, C: M116 .
Shorter-path traverse of rotary axes: M126 .
Reducing display of a rotary axis to a value less than 360°: M94 .
Automatic compensation of machine geometry when working with tilted axes: M114 .
Maintaining the position of the tool tip when positioning with tilted axes (TCPM*): M128 .
Exact stop at corners with nontangential transitions: M134 .
Selecting tilting axes: M138 .
Compensating the machine’s kinematic configuration for ACTUAL/NOMINAL positions at end of block:
7.6 Miscellaneous Functions for Laser Cutting Machines .
Output the programmed voltage directly: M200 .
Output voltage as a function of distance: M201 .
Output voltage as a function of speed: M202 .
Output voltage as a function of time (time-dependent ramp): M203 .
Output voltage as a function of time (time-dependent pulse): M204
8 Programming: Cycles
8.1 Working with Cycles .
Defining a cycle using soft keys
Defining a cycle using the GOTO function .
Calling a cycle .
Working with the secondary axes U/V/W .
8.2 Point Tables .
Creating a point table .
Selecting a point table in the program .
Calling a cycle in connection with point tables .
8.3 Cycles for Drilling, Tapping and Thread Milling .
PECKING (Cycle 1) .
DRILLING (Cycle 200)
REAMING (Cycle 201)
BORING (Cycle 202) .
UNIVERSAL DRILLING (Cycle 203) .
BACK BORING (Cycle 204) .
UNIVERSAL PECKING (Cycle 205) .
BORE MILLING (Cycle 208) .
TAPPING with a floating tap holder (Cycle 2) .
TAPPING NEW with floating tap holder (Cycle 206) .
RIGID TAPPING (Cycle 17) .
RIGID TAPPING (NEW) (Cycle 207) .
THREAD CUTTING (Cycle 18) .
TAPPING WITH CHIP BREAKING (Cycle 209) .
Fundamentals of thread milling .
THREAD MILLING (Cycle 262) .
THREAD MILLING/COUNTERSINKING (Cycle 263) .
THREAD DRILLING/MILLING (Cycle 264) .
HELICAL THREAD DRILLING/MILLING (Cycle 265) .
OUTSIDE THREAD MILLING (Cycle 267) .
8.4 Cycles for Milling Pockets, Studs and Slots .
POCKET MILLING (Cycle 4) .
POCKET FINISHING (Cycle 212)
STUD FINISHING (Cycle 213) .
CIRCULAR POCKET MILLING (Cycle 5) .
CIRCULAR POCKET FINISHING (Cycle 214)
CIRCULAR STUD FINISHING (Cycle 215) .
SLOT MILLING (Cycle 3) .
SLOT (oblong hole) with reciprocating plunge-cut (Cycle 210) .
CIRCULAR SLOT (oblong hole) with reciprocating plunge-cut (Cycle 211) .
HEIDENHAIN iTNC 530
8.5 Cycles for Machining Hole Patterns .
CIRCULAR PATTERN (Cycle 220) .
LINEAR PATTERN (Cycle 221)
Overview of SL cycles .
CONTOUR GEOMETRY (Cycle 14) .
CONTOUR DATA (Cycle 20) .
REAMING (Cycle 21) .
ROUGH-OUT (Cycle 22) .
FLOOR FINISHING (Cycle 23) .
SIDE FINISHING (Cycle 24) .
CONTOUR TRAIN (Cycle 25) .
CYLINDER SURFACE (Cycle 27) .
CYLINDER SURFACE slot milling (Cycle 28) .
8.7 SL Cycles with Contour Formula .
Selecting a program with contour definitions .
Defining contour descriptions .
Entering a contour formula .
Contour machining with SL cycles .
8.8 Cycles for Multipass Milling .
RUN 3-D DATA (Cycle 30) . 330
MULTIPASS MILLING (Cycle 230) .
RULED SURFACE (Cycle 231)
8.9 Coordinate Transformation Cycles
Effect of coordinate transformations
DATUM SHIFT (Cycle 7) .
DATUM SHIFT with datum tables (Cycle 7) .
DATUM SETTING (Cycle 247) .
MIRROR IMAGE (Cycle 8) .
ROTATION (Cycle 10) .
SCALING FACTOR (Cycle 11) .
AXIS-SPECIFIC SCALING (Cycle 26)
WORKING PLANE (Cycle 19) .
8.10 Special Cycles .
DWELL TIME (Cycle 9) .
PROGRAM CALL (Cycle 12) .
ORIENTED SPINDLE STOP (Cycle 13) .
TOLERANCE (Cycle 32) .
9 Programming: Subprograms and Program Section Repeats . 361
Labeling Subprograms and Program Section Repeats .
Programming a subprogram
Calling a subprogram
Program Section Repeats .
Programming a program section repeat
Calling a program section repeat .
Separate Program as Subprogram .
Calling any program as a subprogram .
Types of nesting .
Subprogram within a subprogram .
Repeating program section repeats .
Repeating a subprogram .
HEIDENHAIN iTNC 530
. 10 Programming: Q Parameters
Principle and Overview .
Calling Q parameter functions .
Part Families—Q Parameters in Place of Numerical Values
Example NC blocks .
Describing Contours through Mathematical Operations .
Programming fundamental operations
Programming trigonometric functions .
If-Then Decisions with Q Parameters .
Programming If-Then decisions .
Checking and Changing Q Parameters .
FN14: ERROR: Displaying error messages .
FN15: PRINT: Output of texts or Q parameter values .
FN16: F-PRINT: Formatted output of texts or Q parameter values .
FN18: SYS-DATUM READ Read system data .
FN19: PLC: Transferring values to the PLC .
FN20: WAIT FOR: NC and PLC synchronization .
FN25: PRESET: Setting a new datum .
FN26: TABOPEN: Opening a Freely Definable Table .
FN27: TABWRITE: writing to a freely definable table .
FN28: TABREAD: Reading a Freely Definable Table
Entering Formulas Directly .
Rules for formulas .
10.10 Preassigned Q Parameters .
Values from the PLC: Q100 to Q107 .
Active tool radius: Q108
Spindle status: Q110 .
Coolant on/off: Q111 .
Overlap factor: Q112 .
Unit of measurement for dimensions in the program: Q113 .
Tool length: Q114 .
Coordinates after probing during program run .
Deviation between actual value and nominal value during automatic tool measurement with the TT 130 .
Tilting the working plane with mathematical angles: Rotary axis coordinates calculated by the TNC
Measurement results from touch probe cycles (see also User’s Manual for Touch Probe Cycles) .
11 Test Run and Program Run . 421
Overview of display modes .
Projection in 3 planes .
Repeating graphic simulation .
Measuring the machining time .
Functions for Program Display .
Running a part program .
Moving the machine axes during an interruption
Resuming program run after an interruption .
Mid-program startup (block scan)
Returning to the contour .
Automatic Program Start .
Optional block skip .
Optional Program Run Interruption .
HEIDENHAIN iTNC 530
12 MOD Functions
Selecting the MOD functions .
Changing the settings .
Exiting the MOD functions .
Overview of MOD functions .
Software Numbers and Option Numbers .
Setting the Data Interfaces
Setting the RS-232 interface .
Setting the RS-422 interface .
Setting the OPERATING MODE of the external device .
Setting the BAUD RATE
Software for data transfer .
Connecting the iTNC directly with a Windows PC .
Configuring the TNC .
Configuring PGM MGT .
Changing the setting .
Machine-Specific User Parameters .
Showing the Workpiece in the Working Space
Position Display Types .
12.10 Unit of Measurement .
12.11 Select the Programming Language for $MDI .
12.12 Selecting the Axes for Generating L Blocks
Enter the Axis Traverse Limits, Datum Display
Working without additional traverse limits
Find and enter the maximum traverse .
Displaying HELP Files .
Selecting HELP files .
Display operating times .
. 13 Tables and Overviews
General User Parameters .
Input possibilities for machine parameters .
Selecting general user parameters
Pin Layout and Connecting Cable for the Data Interfaces
RS-232-C/V.24 interface for HEIDENHAIN devices .
Ethernet interface RJ45 socket .
Exchanging the Buffer Battery .
HEIDENHAIN iTNC 530
Introduction
1.1 The iTNC 530


 1.1 The iTNC 530
HEIDENHAIN TNC controls are workshop-oriented contouring controls that enable you to program conventional machining operations right at the machine in an easy-to-use conversational programming language. They are designed for milling, drilling and boring machines, as well as for machining centers. The iTNC 530 can control up to 12 axes. You can also change the angular position of the spindle under program control.
An integrated hard disk provides storage for as many programs as you like, even if they were created off-line. For quick calculations you can call up the on-screen pocket calculator at any time.
Keyboard and screen layout are clearly arranged in such a way that the functions are fast and easy to use.
Programming: HEIDENHAIN conversational and ISO formats
HEIDENHAIN conversational programming is an especially easy method of writing programs. Interactive graphics illustrate the individual machining steps for programming the contour. If a production drawing is not dimensioned for NC, the HEIDENHAIN FK free contour programming does the necessary calculations automatically. Workpiece machining can be graphically simulated either during or before actual machining. It is also possible to program in ISO format or DNC mode.
You can also enter and test one program while the control is running another.
Compatibility
The TNC can run all part programs that were written on HEIDENHAIN controls TNC 150 B and later.